

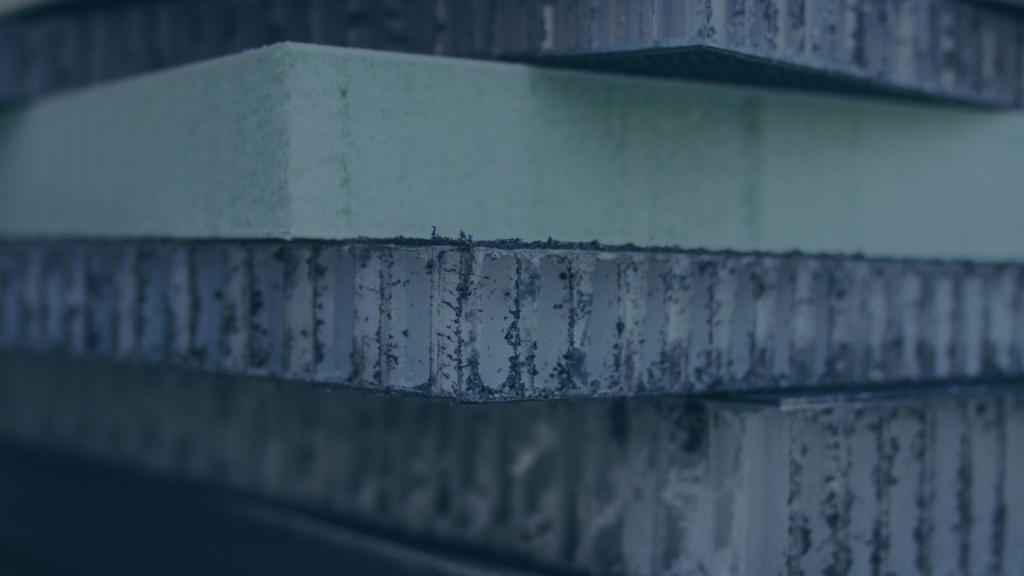
Lightweight composite sandwich panels can be cut, drilled and machined with standard woodworking and metalworking tools, without the need for specialist composite machinery. A circular saw, jigsaw or handheld router fitted with the right blade is enough for most cutting work, while standard drill bits are suitable for fixings. The sections below answer the most common fabrication questions in detail.
Which tools can cut lightweight composite panels?
Standard power tools cut thermoplastic sandwich panels effectively. A circular saw, plunge saw, jigsaw or table saw all work well, provided you use the right blade. For straight cuts in large panels, a plunge saw with a guide rail gives the cleanest result. A router handles rebates, grooves and shaped profiles. CNC routing is the preferred method for large-scale or high-precision work.
In most workshop environments, a circular saw with a fine-toothed blade is the practical starting point. It lets you make straight cuts across the full panel length without fixed machinery. A jigsaw is suitable for curved cuts and internal openings, but requires a lower feed rate to prevent vibration at the cut edge. A handheld router with a straight cutter is useful for edge profiling and for creating rebates for joining systems.
If your production volume justifies it, CNC routing delivers the highest dimensional accuracy and repeatability. For truck body and trailer manufacturers producing consistent panel layouts across multiple build projects, CNC cutting eliminates human variability and significantly increases throughput. Panels are available cut to size to your exact specification, which reduces or eliminates on-site cutting for many standard configurations.
Which saw blade type works best for cutting sandwich panels?
A fine-toothed carbide-tipped saw blade works best for cutting thermoplastic composite sandwich panels. Aim for a blade with at least 60 to 80 teeth for circular saws, and choose a negative or low hook angle to reduce the risk of the blade grabbing the material. Tungsten carbide tips keep their cutting edge longer than standard steel when cutting glass-fibre-reinforced skins.
The glass fibre content of the skins is the main factor determining blade wear. Standard wood-cutting blades dull quickly on glass-fibre-reinforced thermoplastic skins and leave a rougher cut edge. Carbide blades designed for composite or laminate materials stay sharp throughout a full production run and leave a cleaner edge that needs less finishing.
For jigsaws, use a fine-toothed bi-metal or carbide blade with a high tooth count. Feed the saw slowly and let the blade do the work. Forcing the cut causes vibration, which increases the risk of delamination at the cut edge. For routing, use a solid carbide spiral cutter that clears material cleanly from the core without tearing the skin.
How do you prevent delamination when cutting composite panels?
Preventing delamination when cutting sandwich panels depends on three factors: blade sharpness, feed rate and panel support. A sharp blade with a fine tooth count reduces the lateral force on the bond between skin and core. A controlled, even feed rate prevents vibration. Fully supporting the panel on both sides of the cut line stops the offcut from sagging and tearing the skin away from the core.
Masking tape applied along the cut line on both faces of the panel is a simple and effective precaution. The tape holds the surface fibres in place during cutting and reduces chipping on the exit side. Remove the tape carefully after cutting to avoid pulling away surface material.
Panel orientation also matters. When using a circular saw, always cut with the decorative or finished side facing up, because the blade cuts on the upstroke and the exit side is more prone to chipping. With a jigsaw, the blade likewise cuts on the upstroke, so place the finished side facing down. Understanding which side the blade exits from lets you position the panel so that the most important surface is protected.
For thermoplastic panels with a PP honeycomb core, the core itself is relatively forgiving during cutting. The greatest risk lies at the bond between skin and core at the cut edge, which makes support and blade quality more important than cutting speed.
Discuss your project with our team and find out how Compoform can help you with durable sandwich panel solutions.
How are the cut edges of sandwich panels finished and sealed?
Cut edges of sandwich panels must be sealed to protect the core from moisture ingress, UV exposure and mechanical damage. The standard methods are edge banding, edge folding, or applying a compatible sealant or self-adhesive tape. For thermoplastic panels, heat-formed edge banding is the most durable option, because the skin material is wrapped around the cut edge to create a fully closed profile.
For truck body floors and trailer panels that are cleaned regularly with high-pressure water, an unsealed edge is a long-term reliability risk. Water entering a PP honeycomb core through a cut edge does not cause the same rot as in plywood, but it can degrade the bond between skin and core over time and add weight through moisture retention. Sealing the edge eliminates this risk entirely.
For scaffold planks, edge protection is equally important. A panel used as a scaffold plank takes repeated knocks on its edges from boots, tools and adjacent planks. A sealed or banded edge withstands this mechanical wear and maintains the structural integrity of the bond between skin and core throughout the life of the panel. Edge sealing and edge banding are standard finishing steps for Compoform scaffold planks and truck floor panels, not optional extras.
Where heat-formed edge banding is not practical, a two-component structural adhesive or compatible thermoplastic edge tape applied under pressure provides sufficient protection for most indoor or sheltered applications. For outdoor or wash-down environments, heat-formed edges are the more reliable long-term solution.
Can lightweight panels be drilled and fastened without specialist tools?
Yes. Thermoplastic composite sandwich panels can be drilled and fastened using standard drill bits and conventional fasteners. A sharp HSS or carbide drill bit works well for most panel thicknesses. Use low feed pressure and moderate speed to prevent delamination around the hole. Standard rivets, bolts and self-drilling screws fasten effectively into composite panels when used with the correct technique.
The main consideration with sandwich panels is the pull-out strength of fasteners. Because the core material, whether PP honeycomb or PET foam, carries less compressive load than a solid material, point loads from fasteners concentrate on the skin. For structural connections, use a washer or backing plate to spread the load over a larger skin area. You can also fit a solid plug or potted insert into the core at the fixing location before drilling.
For through-bolted connections, drill cleanly through both skins and the core, then fit a sleeve or grommet to prevent the fastener from crushing the core under torque. This is standard practice for trailer floor connections and body mounting points where vibration loads are continuous.
Self-drilling screws work well for lighter fixings such as interior finishing, cable management or panel-to-panel joining strips. Drive them in at low speed to avoid damaging the core material around the thread. Pre-drilling to the correct diameter for the screw shank gives a cleaner thread engagement and better pull-out resistance than driving directly into an undrilled panel.
What are the most common mistakes when machining composite panels?
The most common fabrication mistakes with sandwich panels are using the wrong blade, cutting too fast, failing to seal edges and under-designing fastener connections. Each of these mistakes is avoidable with proper preparation, and each has a direct consequence for panel performance or service life.
- Using a coarse or worn blade: Coarse teeth tear rather than cut through the glass-fibre-reinforced skin, producing a ragged edge and increasing the risk of delamination. Replace blades regularly and match the tooth count to the panel skin specification.
- Cutting too fast: A high feed rate generates heat and vibration, both of which weaken the bond between skin and core at the cut line. Slow down and let the blade work at its own pace.
- Leaving cut edges open: An unsealed edge exposes the core to moisture and mechanical damage. This is the most common cause of premature panel failure in transport and scaffold plank applications.
- Ignoring panel orientation during installation: Panels with cross-ply skins perform equally in both directions, so orientation is flexible. However, panels with direction-optimised construction, such as scaffold planks designed for transverse loading, must be installed in the correct orientation to deliver their rated performance.
- Under-designing fastener connections: Using fasteners without load distribution on the skin leads to pull-out failure under dynamic or repeated loading. Always allow for the lower compressive strength of the core when designing connection points.
- Assuming all panels are machined the same way: Floor panels with a PP honeycomb core behave differently from wall panels with a PET foam core. Blade choice, feed rate and edge treatment should be matched to the specific panel construction, not applied as a single universal method.
How Compoform helps with panel cutting and machining
We supply panels cut to size to your exact dimensions, which removes most on-site cutting from your production process. Our semi-automatic production line handles panels up to 13,500 mm × 2,950 mm, so we can match your body or trailer dimensions directly rather than forcing you to cut down a standard sheet.
Beyond dimensions, we work with you before production to review your fabrication process and flag potential problems:
- We advise on edge treatment options — heat-formed edge banding, edge banding or sealant — based on your application environment and wash conditions.
- We review fastener connection designs and recommend insert or potting solutions where pull-out loads are a concern.
- We confirm the panel orientation requirements for every direction-optimised construction, so your assembly team installs panels correctly from day one.
- For truck floor applications, we can supply self-supporting 30 mm PP sandwich panels that eliminate the aluminium subframe, removing a production step and lowering your total build cost.
- Thermoplastic composite floors last significantly longer than plywood in heavy-duty transport applications. Over a vehicle life of 15 years, that eliminates multiple replacement cycles. When you factor in panel costs, installation labour and vehicle downtime, the composite delivers a lower cost per year of service, even at a higher unit price.
If you are specifying panels for electric truck or van bodies, weight reduction has a second argument alongside payload. Every kilogram saved in the body structure increases battery range per charge. In 2026 this is a standard purchasing question from EV fleet buyers, and it strengthens the case for composite floors and walls over steel or timber alternatives. Explore composite panel applications across different sectors to see how other industries use lightweight sandwich panels.
We review your design, optimise the panel layout for your assembly process, and stay involved during integration and with any issues after delivery. See how this works for truck body applications. Contact our composite panel fabrication team to discuss your project requirements.
Related Articles
- How does lightweight formwork affect transport efficiency?
- How do biobased sandwich panels compare to conventional sandwich panels?
- What is the procurement process for sandwich panels in high-volume manufacturing?
- How thick should sandwich panels be in a motorhome build?
- Which industries benefit most from switching to sandwich panels?