

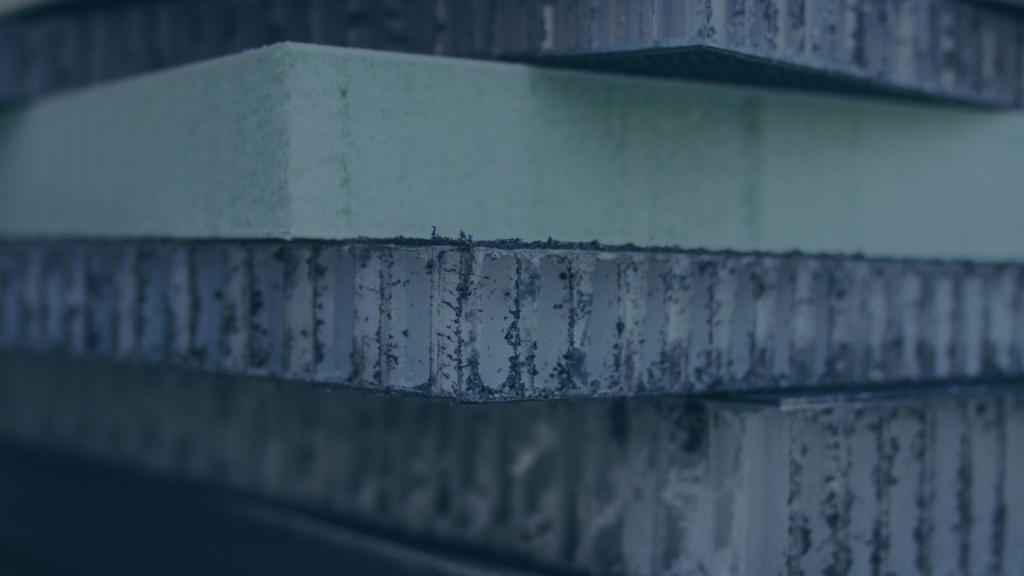
A sandwich panel can carry substantial structural loads while weighing only a fraction of what steel or solid composite would require. The exact load-bearing capacity depends on the panel’s thickness, core material, skin specification and span, so there is no universal figure. The sections below cover the key variables, from construction principles to real-world testing, so you can match the right panel specification to your application.
What factors determine how much load a sandwich panel can carry?
The load-bearing capacity of a sandwich panel is determined by four primary factors: panel thickness, core material and density, skin type and construction, and the span over which the panel is supported. Change any one of these variables and the load-bearing result changes significantly. No single figure covers all configurations; it is the combination of these factors that determines performance.
Thickness has a disproportionate effect on bending stiffness. Doubling a panel’s thickness does not simply double its bending resistance but increases it by a much larger factor, because the skins move further from the neutral axis, where bending stress is highest. This is why a 30 mm floor panel carries considerably higher absolute loads than a 15 mm panel of identical construction.
Core density determines compressive strength and shear resistance. A denser core resists point loads and distributes them more effectively across the panel surface. A 140 kg/m³ PP honeycomb core, for example, offers noticeably higher compressive strength than a 120 kg/m³ honeycomb of the same geometry, which matters when the panel must absorb concentrated loads from feet, wheels or equipment.
Skin specification determines tensile and flexural performance. The number of layers, fibre orientation and glass content all influence how much bending stress the skins can absorb before failure. A skin with 4 layers of glass fibre carries more load than a skin with 2 layers, and a cross-ply layup distributes strength more evenly across directions than a unidirectional layup.
Span is the variable most often underestimated. A panel that performs well over a short span may deflect excessively or fail over a longer unsupported span. Load-bearing calculations should always refer to the actual support distance in the final assembly.
How does sandwich panel construction affect structural strength?
Sandwich panel construction achieves high structural strength by separating two stiff, strong skins with a lightweight core. The skins absorb tensile and compressive bending stresses, while the core resists shear forces and keeps the skins apart. This geometry produces a structure that is considerably stiffer and stronger relative to its weight than a solid panel of the same material.
The principle is similar to an I-beam in steel construction: placing material at the outer faces, where bending stresses are highest, maximises efficiency. The core does not need to be as strong as the skins; its role is to maintain the distance between the skins and to transfer shear loads. This is why a low-density foam or honeycomb core can be structurally effective, even though it would fail immediately under direct load without the skins.
The bond between skin and core is equally important. If the skin-to-core bond fails through delamination caused by impact, moisture ingress or thermal cycling, the panel loses its composite action and its load-bearing capacity drops sharply. Edge sealing and the quality of the skin bond are therefore not cosmetic details but structural requirements, particularly in applications where panels are regularly washed down or exposed to outdoor conditions.
Core geometry also plays a role. A honeycomb core distributes compressive loads through its cell walls, making it well suited to floor panels that must handle point loads from pallets or equipment. A foam core distributes load more evenly through its volume, which suits wall panels where the primary loads are lateral pressure and wind rather than concentrated point loads.
How do composite sandwich panels compare with steel and aluminium in load-bearing capacity?
Composite sandwich panels do not match steel or aluminium in absolute load-bearing capacity per unit of area, but they match or exceed them in load-bearing capacity per unit of weight. For most transport and scaffold platform applications, the relevant measure is structural performance relative to mass, not raw strength. On that basis, composite panels consistently outperform both metals.
Steel is heavy. A steel floor panel strong enough for use in trailers adds considerable dead weight to the vehicle structure. Every kilogram of structural dead weight is a kilogram that cannot carry cargo, and in 2026 it is also a kilogram that reduces the battery range of electric trucks and vans. Buyers of electric fleets now treat structural weight as a range argument, not just a payload argument. Lighter body structures extend range per charge, which is a direct procurement consideration when specifying vehicle bodies.
Aluminium is lighter than steel but still heavier than a well-specified composite panel, and it corrodes in certain environments, requires subframe support in many floor applications and is more expensive to repair after impact damage. A 30 mm thermoplastic sandwich floor panel is self-supporting; no aluminium subframe is needed, which eliminates a production step and lowers costs for truck body builders.
Composite panels also resist fatigue better than metals under repeated dynamic loading, which is relevant for trailer floors and vehicle bodies that are loaded and unloaded thousands of times over a vehicle’s lifetime.
Discuss your project with our team and find out how Compoform can help you with durable sandwich panel solutions.
What types of loads must sandwich panels handle in practice?
In practice, sandwich panels face four main types of load: distributed loads spread across the panel surface, point loads concentrated in a small area, dynamic or impact loads from sudden forces, and shear loads acting parallel to the panel plane. Most applications involve a combination of these at the same time.
Distributed loads are the most common in floor applications: the weight of cargo spread across a trailer floor or the weight of workers and materials on a scaffold plank. These loads test the panel’s bending stiffness and its ability to resist deflection over a span.
Point loads are more demanding per unit of area. A forklift wheel, a pallet corner or a scaffold clamp concentrates force in a small contact area. The compressive strength of the core and the local stiffness of the skin determine whether the panel dents or holds. A 140 kg/m³ honeycomb core is specifically suited to these conditions in floor panels.
Impact loads occur when objects are dropped or when a vehicle body is struck. Thermoplastic composite panels absorb impact energy through deformation of the fibre-reinforced skins rather than cracking or breaking, which is a meaningful advantage over brittle materials in operational environments.
Shear loads act along the panel plane, relevant in wall panels subject to wind pressure or in structural panels used in vehicle bodies where the panel contributes to the overall stiffness of the structure. The core must transfer these forces between the skins without failing in shear.
How is the load-bearing capacity of sandwich panels tested and certified?
The load-bearing capacity of sandwich panels is tested through standardised mechanical tests that measure flexural strength, flexural modulus, compressive strength and tensile properties. In Europe, the relevant standards are ISO 14125 for flexural testing and EN ISO 844 for compressive properties. For scaffold platform applications, EN 12811 defines load classes that panels must meet to be used on construction sites.
Flexural tests use a three-point bending setup: the panel specimen is supported at two points and loaded in the centre until failure. This yields values for flexural strength (how much stress the panel withstands before fracture) and flexural modulus (how stiff the panel is under load). These values are measured across multiple specimens to establish a reliable average and a minimum performance threshold.
Compression tests measure how much force the core resists when loaded perpendicular to the panel plane, which is directly relevant to point-load performance in floor panels. Tensile tests of the skins, carried out in both the 0° and 90° fibre directions, confirm that the skins can carry the bending stresses the panel will experience in service.
For scaffolds, EN 12811 load class certification is the standard European benchmark. A panel that achieves load class 4 under EN 12811 with no support underneath has demonstrated a specific, verified load-bearing capacity, not a theoretical estimate. This type of certified test result is what procurement engineers and site safety managers require before specifying a panel for scaffold applications.
Published technical datasheets state minimum performance values, which are typically conservative relative to average test results. This built-in safety margin is deliberate; it ensures that panels in service perform above the stated minimum, even with normal production variation.
When should a custom panel specification be used instead of a standard size?
A custom panel specification is appropriate when a standard panel does not meet the structural, dimensional or weight requirements of your specific application. In practice, this applies to most serious OEM and specialist manufacturing projects, because the load case, span and mounting constraints of a truck body floor or a scaffold system rarely match off-the-shelf dimensions and configurations perfectly.
The most common reasons to move to a custom specification are:
- Non-standard dimensions: Standard panels may not cover the required length or width without joints. Panels are available in custom sizes cut to your exact specification, including lengths up to 13,500 mm, which eliminates mid-panel joints that create weak points and add assembly time.
- Specific load requirements: If your application involves unusually high point loads, a longer unsupported span or a demanding dynamic load cycle, a standard panel may be over- or under-dimensioned. A custom skin layup or core density can match the panel to the actual load case.
- Weight targets: If you are working towards a specific payload or range target, particularly relevant for electric truck bodies where every kilogram of structure affects range per charge, a custom specification lets you optimise the panel for the minimum weight that still meets the structural requirement.
- Surface or edge requirements: Anti-slip surfaces, specific edge profiles or edge sealing for moisture resistance may not be available in standard configurations, but are straightforward to specify in a custom panel.
The decision between standard and custom ultimately comes down to whether the performance gap between what a standard panel delivers and what your application requires is worth the additional specification work. For mid-sized OEM production runs, the answer is usually yes, because the panel specification is repeated across every unit produced, and an optimised panel lowers the total cost of ownership across the entire fleet or product line.
How we help you specify the right sandwich panel
We work with truck body builders, trailer manufacturers and scaffold companies to define panel specifications that match the actual load requirements of their applications, not generic configurations that approximate the need.
This is what that process looks like in practice:
- Load case assessment: We review your structural requirements, span, load type, point load locations and safety factors, and recommend a core density, skin layup and thickness that meet them without over-specifying the panel.
- Dimension optimisation: We produce panels in custom sizes to eliminate unnecessary joints and simplify your assembly process. For truck body floors, this often means one panel per bay instead of multiple panels joined on site.
- Test data and certification support: We provide test data referencing European standards (ISO 14125, EN ISO 844, EN 12811), so your engineering team has verified performance figures, not estimates. For scaffold platform applications, we can supply panels tested to EN 12811 load class requirements.
- Compatibility with electric fleets: If you build bodies for electric trucks or vans, we help you quantify the weight saving compared with steel or plywood and translate it into range and payload terms for your customers’ procurement teams.
- Lifecycle cost framing: Over a vehicle lifetime of 15 years, a composite floor eliminates two to three plywood replacement cycles. When you account for panel cost, installation labour and vehicle downtime, the composite is cheaper per year of service, even at a higher unit price. We help you build that argument for your own customers.
We treat every project as a technical partnership, not a transaction. That means reviewing your design, flagging integration issues before production begins, and staying involved during the first production run. If you are specifying panels for a new vehicle body or a scaffold system, talk to our application engineers about your load requirements and we will work with you to develop the right configuration.
Related Articles
- What are the disadvantages of switching from plywood to composite formwork?
- How do composite and plywood panels compare in dimensional stability?
- How much does aluminium really cost over its lifetime?
- Why is PP honeycomb used as a core material in sandwich panels?
- What sandwich panels are used in caravan walls and roofs?