

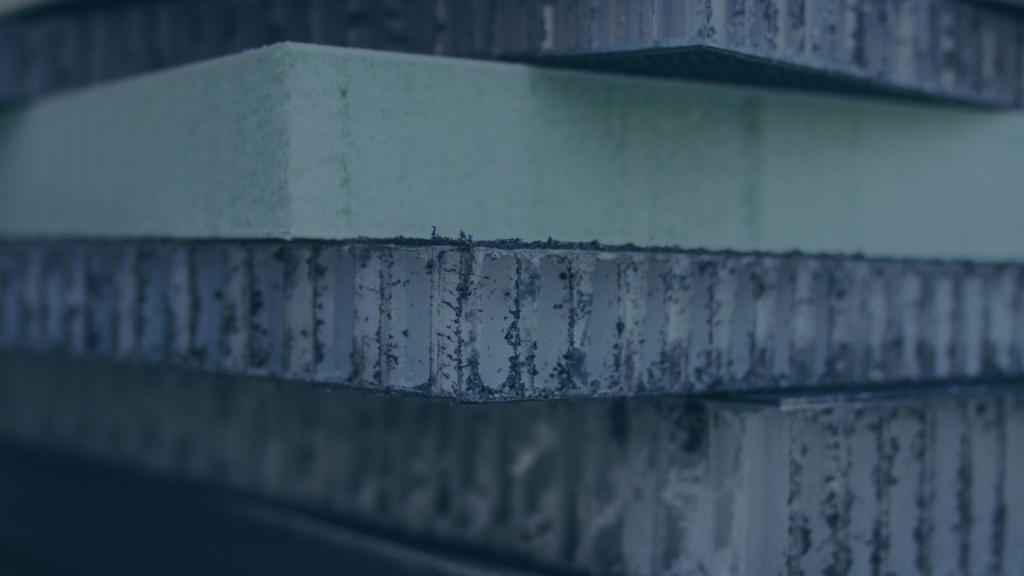
This article covers the broader sandwich panel market. Compoform’s range is limited to PP honeycomb cores and PET foam cores for commercial vehicles and scaffolding.
The core in a sandwich panel carries shear forces between the two skins, keeps those skins at a fixed distance from each other, and resists pressure perpendicular to the panel surface. Without a structurally capable core, the skins buckle independently of one another and the panel loses most of its load-bearing capacity. The sections below answer the most frequently asked technical questions about core materials, from their influence on stiffness to which type performs best under impact.
How does the core material affect the stiffness of a sandwich panel?
The core material determines the bending stiffness of a sandwich panel by controlling how far apart the two skins are held and how effectively shear forces are transferred between them. A stiffer, denser core holds the skins together as a single unit, so the structural contribution of the skins is far greater than what either skin could achieve on its own.
The structural logic resembles that of an I-beam: the flanges (skins) carry tensile and compressive stresses, while the web (core) transfers the shear forces. If the web is weak or soft, the flanges bend independently of each other and the beam fails. In a sandwich panel, a core that deforms under shear load lets the skins slide relative to one another, which destroys the bending stiffness — even if the skins themselves remain intact.
Core thickness also plays a direct role. Increasing the panel thickness by increasing the core depth raises the bending stiffness considerably, because stiffness scales with the cube of the distance between the centroids of the skins. This is why relatively thin skins bonded to a thick, lightweight core can outperform a much heavier solid plate in bending resistance per unit of weight.
What types of core materials are used in composite sandwich panels?
In the broader sandwich panel market, the most commonly used core materials are polymer foams, honeycomb structures, and natural or engineered solid materials. Each category offers a different balance of density, shear strength, compressive resistance, and cost. The right choice depends on the load type, the service environment, and the production method.
Polymer foam cores are the most widely used category. Polypropylene (PP) foam and PET foam are thermoplastic options that combine low density with good compressive and shear properties. They are compatible with thermoplastic production processes and fully recyclable, which is becoming increasingly relevant under the EU End-of-Life Vehicles (ELV) Directive for commercial vehicle manufacturers and their applications.
Honeycomb cores are structured cell patterns, typically hexagonal, that offer a very high stiffness-to-weight ratio. PP honeycomb is a thermoplastic option used in demanding structural applications such as truck body floors and scaffold boards, where compressive strength and shear resistance under point loads are the priority.
Other core types on the market include balsa wood, aluminium honeycomb, and mineral wool, but these are tied to specific sectors such as marine, aerospace, and fire-resistant building panels, and are not part of every manufacturer’s range.
How does core density affect panel weight and load-bearing capacity?
A higher core density increases both the weight of the panel and its structural capacity. A denser core contains more material per unit of volume, which raises compressive strength, shear strength, and resistance to local indentation. The trade-off is a heavier panel, so selecting the right density means matching the structural requirements to the minimum weight that satisfies them.
For truck body builders and trailer manufacturers, this trade-off has direct commercial consequences. Every kilogram of structural dead weight in a vehicle body reduces the payload available for revenue-generating cargo. For electric trucks and vans, the impact goes further: heavier body structures reduce battery range per charge, which in 2026 is a standard question when procuring EV fleets. Weight reduction is no longer just a payload argument — it is a range argument too.
PP foam cores, for example, are available in a range of densities. Lower-density foam is suitable for wall linings where compressive loads are limited. Higher-density foam or PP honeycomb is specified for floor panels and scaffold boards, where point loads and repeated dynamic loads demand greater compressive resistance. Selecting the lowest density that meets the structural requirement keeps the panel as light as possible without compromising performance.
Discuss your project with our team and find out how Compoform can help you with durable sandwich panel solutions.
What happens to a sandwich panel when the core fails?
When the core of a sandwich panel fails, the panel loses its ability to transfer shear forces between the skins, and the two skins begin to act as independent thin plates rather than as a composite structure. This causes a sudden and dramatic loss of bending stiffness, often followed by visible wrinkling or buckling of the compressed skin.
Core failure can take several forms, depending on the load type and the core material:
- Shear failure occurs when the core cannot transfer the shear forces generated by bending. The skins slide relative to one another and the panel deflects far beyond its design limit.
- Compressive failure occurs under concentrated point loads, such as a footstep on a scaffold board or a fork tip on a truck floor. The core is crushed locally, causing permanent indentation and reducing the panel’s load-bearing capacity in that area.
- Delamination is the detachment of the skin from the core at the bond line. Once a skin comes loose, it no longer contributes to the structural performance of the panel, even though the skin itself is undamaged.
In practice, well-designed sandwich panels are built so that the core and the skin fail at comparable load levels, avoiding a situation in which one element is significantly oversized relative to the other. For scaffolding applications in particular, resistance to local compressive failure is a primary design criterion, because workers and equipment create concentrated loads across the surface of the board.
How does core material selection differ between thermoplastic and thermoset sandwich panels?
The choice of core material is closely tied to the production process. Thermoplastic sandwich panels are produced using heat and pressure, which means the core must withstand the processing temperatures without degrading. Thermoset panels are cured at lower temperatures with resins, which opens the door to a wider range of core materials that cannot withstand thermoplastic processing conditions.
In thermoplastic panels, PP honeycomb and PET foam are the standard core options. Both materials are compatible with the heat and pressure of thermoplastic lamination, and both are fully recyclable at the end of their service life. This recyclability is a compliance consideration for European OEMs covered by the EU End-of-Life Vehicles (ELV) Directive, which requires vehicle manufacturers to demonstrate that a large share of vehicle materials can be recovered and recycled.
Thermoset panels, by contrast, are often produced with balsa wood, aluminium honeycomb, or other materials suited to lower-temperature curing processes. However, thermoset panels are not recyclable in the same way, because the resin matrix cannot be remelted and reprocessed. For manufacturers facing growing pressure under the EU Corporate Sustainability Reporting Directive (CSRD), this distinction is becoming an increasingly active factor in material choices.
The practical implication for truck body builders and trailer manufacturers is that thermoplastic panels offer a recyclability advantage that thermoset alternatives cannot match, without sacrificing structural performance in the applications they are specified for.
Which core material is best for high-impact applications?
For high-impact applications, PP honeycomb cores consistently outperform foam cores in compressive strength and resistance to local impact damage. The structured cell geometry of a honeycomb distributes impact energy across multiple cell walls, which limits the depth and spread of damage compared with a foam core of equivalent density.
In scaffold boards and truck body floors — two of the most demanding impact environments in commercial applications — PP honeycomb provides the compressive resistance needed to withstand repeated point loads without permanent deformation. The skin architecture also plays a role: a triaxial glass fibre composition (such as a 90-0-90 configuration) distributes tensile loads in multiple directions, which improves the panel’s ability to absorb and spread impact forces rather than concentrating them at a single point.
Skin reinforcement technology raises the limit of impact performance further. Continuous fibre-reinforced tape, for example, delivers a considerably higher impact resistance than standard composite skins, making it relevant for applications where impact events are frequent or severe.
The right answer for a specific application depends on the nature of the impact (distributed versus point load), the load frequency, and the acceptable level of permanent deformation. A scaffold board must survive repeated foot traffic and dropped tools without visible damage. A truck floor must withstand fork-tip loads and pallet drops over a service life of years, not months.
How does Compoform support core selection for your application?
We work with two core materials — PP honeycomb and PET foam — specified in a range of densities to meet the structural and weight requirements of your application. Rather than offering a standard panel and asking you to adapt your design around it, we review your load requirements, service environment, and assembly procedure before recommending a configuration.
For truck body builders and trailer manufacturers, this typically means:
- Selecting the core density to meet floor load requirements while keeping panel weight as low as possible — which contributes directly to payload and, for electric fleets, battery range per charge
- Specifying the skin architecture (cross-ply, 2-layer, or 4-layer glass fibre) to match the direction and magnitude of the loads your panels will carry
- Producing panels in custom dimensions up to 13,500 mm × 2,950 mm, eliminating joints that create weak points in large floor or wall assemblies
- Applying edge sealing and edge bending where panels are exposed to cleaning cycles or outdoor conditions, protecting the core from moisture ingress throughout the service life of the panel
For scaffold manufacturers, we can point to our own test data: a 10.5 mm Compoform panel achieved EN 12811 load class 4 with no support beneath it — a result that comes from the combination of PP honeycomb core thickness, skin composition, and panel geometry working together, not from any single element in isolation.
If you are specifying a panel for a new application or revising an existing design, talk to our engineering team about the load case, and we will work through the core and skin configuration with you before anything goes into production.
Related Articles
- How are sandwich panels used in ground support equipment?
- What are the slip resistance properties of sandwich panel scaffold boards?
- What are the weight savings of switching to sandwich panels in a trailer?
- What is the strength-to-weight ratio of a sandwich panel?
- How to evaluate panel materials for weight-sensitive applications?