

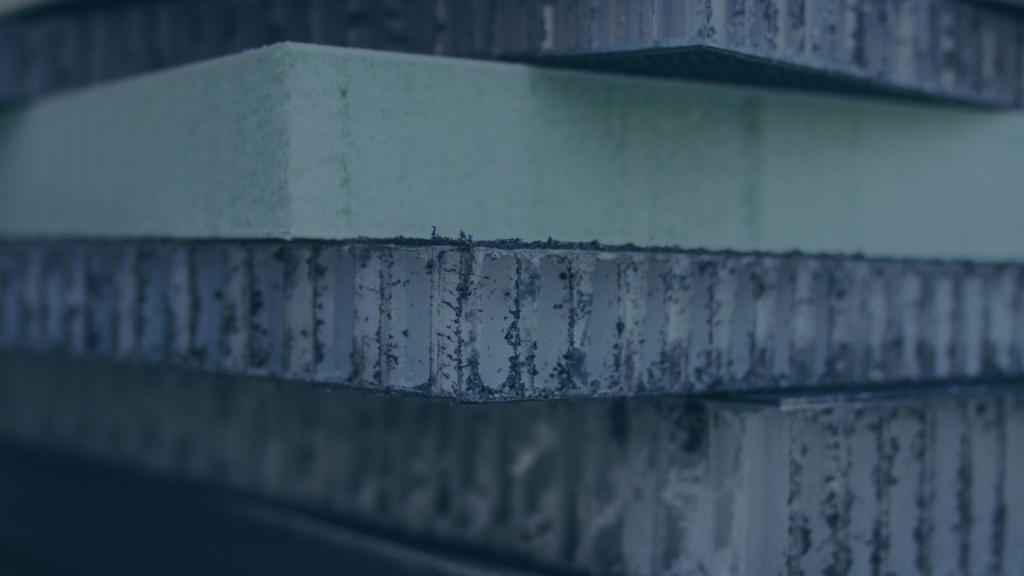
A double belt press is a continuous lamination machine that bonds multiple material layers under controlled heat and pressure into flat, uniform composite panels. Two opposing steel belts move in synchrony and apply a constant force across the full panel width as the materials pass through a heating zone and then a cooling zone. The result is a fully consolidated sandwich panel produced in one uninterrupted process. The sections below answer the most common questions about how this technology works and why it matters for composite panel manufacturing.
How does a double belt press actually work?
A double belt press works by feeding raw materials between two continuous steel belts that run parallel to each other. The belts apply even pressure across the entire panel surface as the assembly passes through a heating zone that activates the thermoplastic matrix, followed by a cooling zone that locks the consolidated structure in place. The process runs continuously and produces panels at a constant rate without intermediate stops.
The heating zone raises the temperature of the thermoplastic skins and the core to the point where the polymer flows and bonds to adjacent layers. The belt pressure ensures intimate contact between skin and core, eliminating voids and delamination risks. When the panel leaves the heating zone, the cooling section brings the temperature down rapidly, fixing the bond before the panel exits the press.
Pressure control across the belt width is what sets a well-designed double belt press apart from simpler lamination equipment. Uneven pressure causes thickness variation and internal stress. A correctly calibrated press maintains a uniform nip pressure from edge to edge, so panels produced this way show consistent mechanical properties across their entire surface.
Which materials can be processed in a double belt press?
A double belt press can process a wide range of thermoplastic and thermoset-compatible materials, provided they can be consolidated in a continuous format under heat and pressure. Common skin materials include glass-fibre-reinforced polypropylene (glass-fibre PP), carbon-fibre PP, plain PP films and glass-PET laminates. Core materials include PP foam, PP honeycomb and various other lightweight structural cores.
The press can also process surface films and functional layers in-line. PET films, anti-slip coatings and decorative finishes can be laminated directly onto the panel surface during the same pass, removing the need for a secondary bonding step. This in-line capability is one of the reasons continuous pressing is preferred over batch methods for high-volume production.
The choice of material determines the required temperature and pressure profile. PP-based systems are typically processed at lower temperatures than PET-based systems. The press must be able to hold the correct temperature window precisely, because too little heat leaves the bond incomplete, while too much heat degrades the polymer or distorts the core geometry. This is why process control, not just machine size, determines output quality.
What types of panels does a double belt press produce?
A double belt press produces flat, continuous sandwich panels with a lightweight core bonded between two reinforced skin layers. The specific panel type depends on the combination of core material, skin architecture and surface finish fed into the press. Common products include wall cladding, structural floor panels, scaffold planks and body panels for commercial vehicles and trailers.
The core geometry determines the structural role of the panel. PP foam cores, available in a range of densities, suit wall panels and applications where thermal insulation or a smooth surface matters. PP honeycomb cores deliver higher bending and compression performance at the same thickness, making them the preferred choice for floor panels and load-bearing floors in transport applications.
The skin architecture provides further differentiation. A cross-ply laminate, with fibres oriented at 0 and 90 degrees in alternating layers, delivers balanced mechanical properties in both directions, which suits panels that may be installed in either orientation. A unidirectional multilayer skin concentrates strength along a specific axis, which is useful when the dominant load direction is known, as with scaffold planks loaded across their width.
Discuss your project with our team and find out how Compoform can help you with durable sandwich panel solutions.
How does a double belt press compare with batch lamination methods?
A double belt press produces panels continuously, whereas batch lamination methods press one panel at a time in a static mould or platen press. The continuous process delivers higher throughput, more consistent bond quality and lower cost per unit at scale. Batch methods offer more flexibility for small runs, complex shapes or materials that require very long dwell times under pressure.
Consistency is the most significant practical difference. In a batch press, every cycle introduces variables: loading position, platen temperature uniformity and clamping pressure can all shift slightly between cycles. A continuous belt press eliminates these cycle-to-cycle variables because the process parameters stay constant as long as the line is running. For OEM manufacturers producing the same panel specification in volume, this consistency directly reduces reject rates and rework.
Batch lamination remains relevant for prototyping, low-volume specialty panels and configurations that require very thick cores or complex edge profiles that a continuous press cannot handle. For high-volume production of flat sandwich panels, however, the double belt press is the more productive and cost-effective process, particularly when panel dimensions and material combinations are standardised.
Why do composite panel manufacturers use a double belt press?
Composite panel manufacturers use a double belt press because it combines high production volume with tight process control, producing panels that meet consistent mechanical and dimensional tolerances at a cost that batch methods cannot match at scale. The continuous format also allows in-line integration of surface films, core materials and reinforcement layers, reducing the number of separate production steps.
For manufacturers supplying truck body builders, trailer producers and other commercial vehicle OEMs, consistency is not optional. A panel whose thickness varies by even a few tenths of a millimetre causes fit problems during assembly. A panel with inconsistent skin-to-core bonding creates warranty risk. The double belt press addresses both risks through continuous, controlled consolidation.
There is also a weight argument. Thermoplastic sandwich panels produced on a double belt press replace steel and wood in vehicle body structures at a fraction of the weight. In 2026 this matters beyond payload alone. Lighter body structures extend the battery range of electric trucks and vans. Every kilogram of structural dead weight reduces range per charge, making weight reduction a range argument, not just a payload argument. This is a standard procurement question for EV fleet buyers, and it makes the case for composite panels stronger than ever.
What panel dimensions can a double belt press achieve?
The panel dimensions of a double belt press depend on the belt width and the cutting system downstream of the press. The width is set by the machine design, while the length is theoretically unlimited in a continuous process and is determined by the downstream cutting equipment. The thickness is controlled by the gap between the belts and typically ranges from a few millimetres to around 150 mm, depending on the press configuration.
Large-format panels are one of the practical advantages of continuous pressing. A press wide enough to produce panels nearly three metres wide can supply truck body builders and trailer producers with one-piece floor or wall panels that eliminate internal joints. Fewer joints mean fewer potential points of failure and faster assembly on the production line.
Panel length is particularly relevant for vehicle body applications. A trailer floor or a truck body side wall often requires a panel longer than a batch press can produce in a single cycle. A continuous press, combined with a downstream saw or guillotine, can cut panels to any specified length without restarting the process, which is why long-format panels are produced almost exclusively on continuous equipment.
How Compoform supports your panel specification
We operate a 72-metre semi-automatic double belt press line at our facilities in the Netherlands, capable of producing thermoplastic sandwich panels up to 13,500 mm long and 2,950 mm wide, with thicknesses up to 150 mm. Our annual production capacity reaches 1.5 million square metres of composite sheet material, all manufactured in Europe to consistent quality standards.
What this means in practice for truck body builders, trailer producers and scaffold manufacturers:
- Custom-cut dimensions to your specification — panels are not limited to standard sheet sizes. If your assembly process requires a specific length or width, we produce to that size.
- PP honeycomb and PP foam cores in a range of densities, matched to your load requirements and weight targets. A 30 mm PP sandwich floor panel is self-supporting, which removes the need for an aluminium subframe and eliminates a production step from your build process.
- Thermoplastic panels that significantly outlast plywood in heavy-duty transport applications, based on our own field experience. Over a vehicle lifetime of 15 years, eliminating two or three plywood replacement cycles changes the total cost calculation considerably, even when the composite panel has a higher unit price.
- EN 12811 load class 4 performance achieved by our 10.5 mm scaffold plank panel without support underneath, based on Compoform’s own testing.
- Edge sealing and edge bending available to protect the core from moisture and UV exposure, relevant for scaffold planks and truck floors that are washed down regularly.
We review your design before production begins. If a panel configuration creates an assembly problem, a structural risk or an unnecessary cost, we flag it in the engineering phase, not after the first production run. For scaffold and commercial vehicle floor applications in particular, contact our team to discuss your panel and let us confirm the right configuration for your build process.
Related Articles
- Why is traditional material weight hurting your vehicle's fuel costs?
- Why is steel no longer the default choice for vehicle body construction?
- What is GRP and when is it used as a sandwich panel face sheet?
- How do sandwich panels meet aerospace weight and strength requirements?
- What is the difference between continuous and batch lamination?